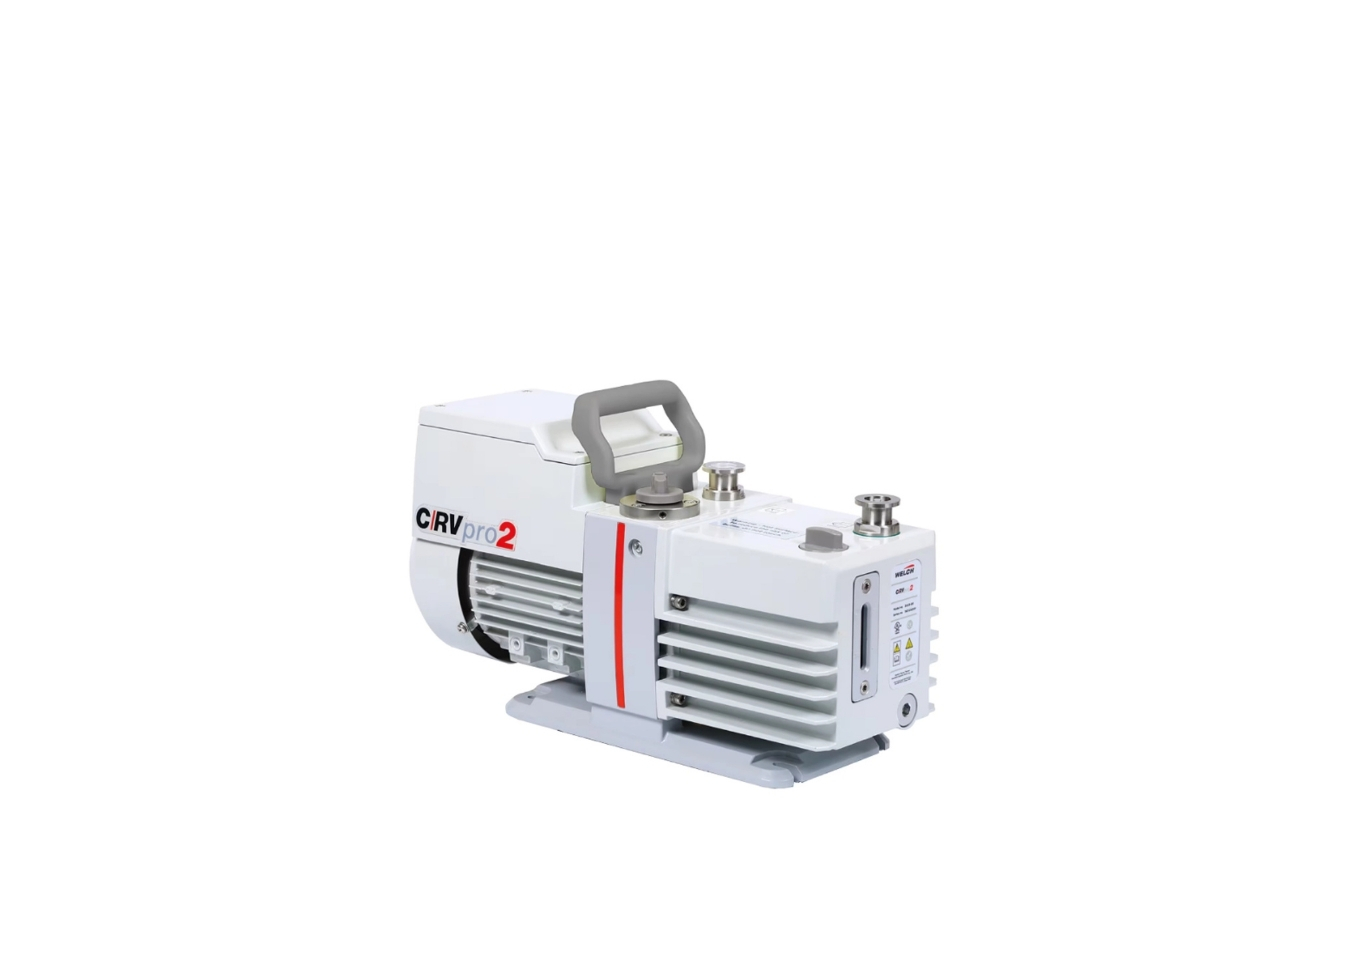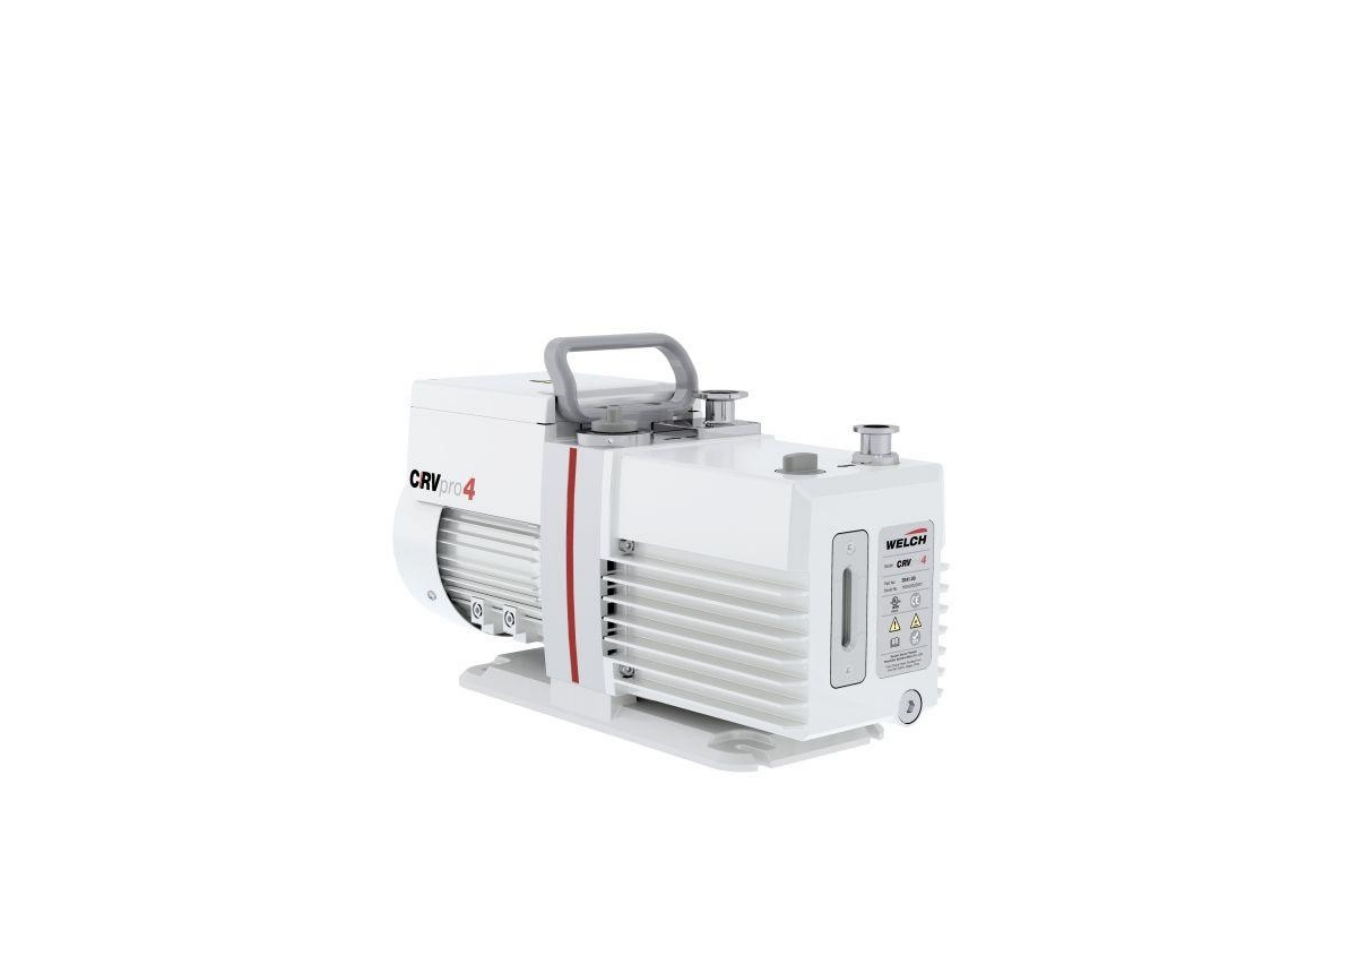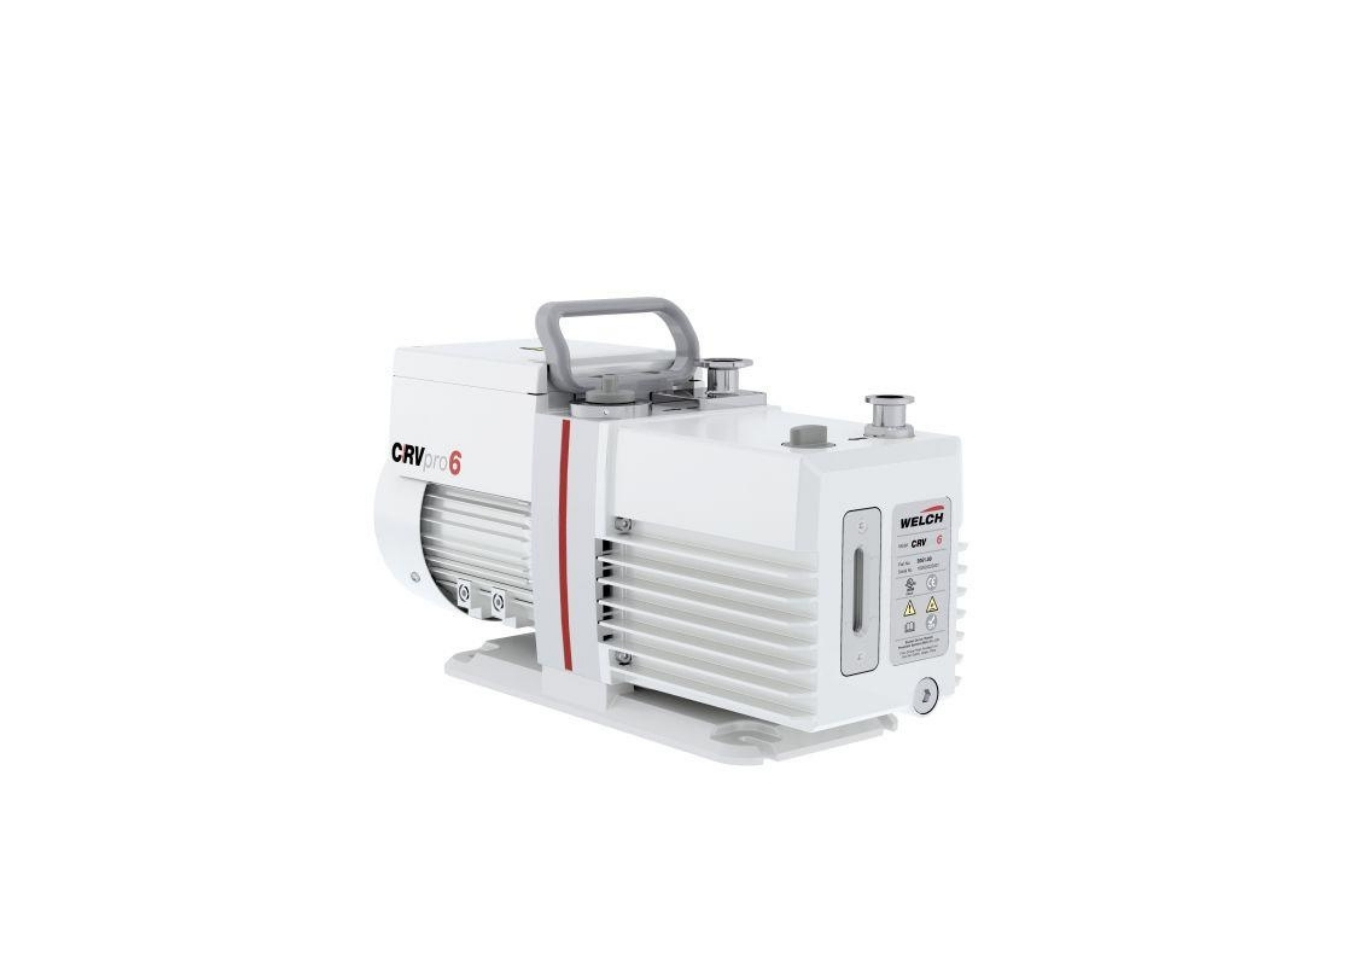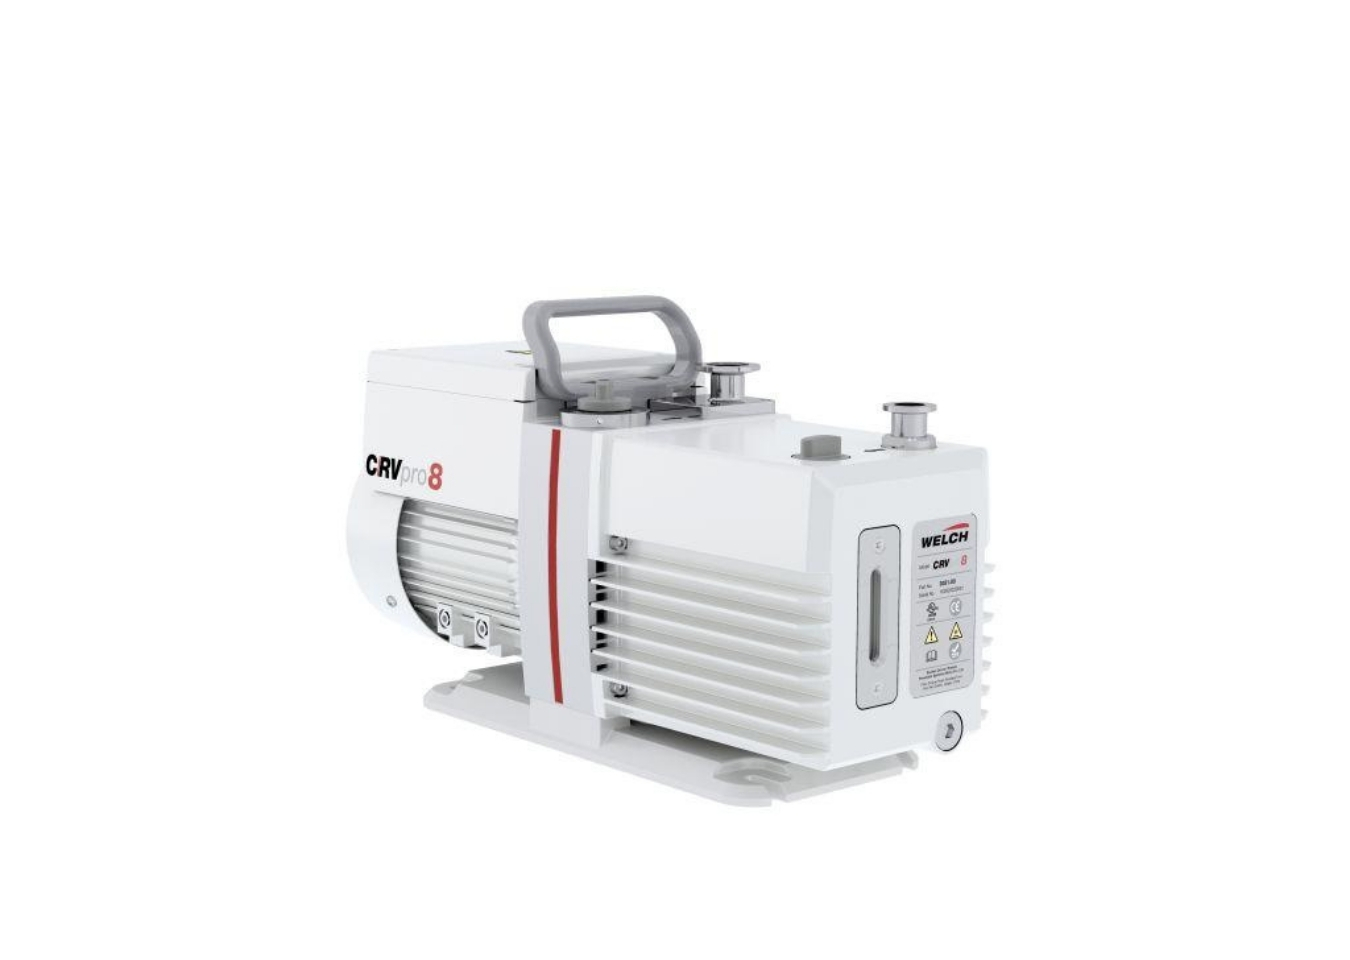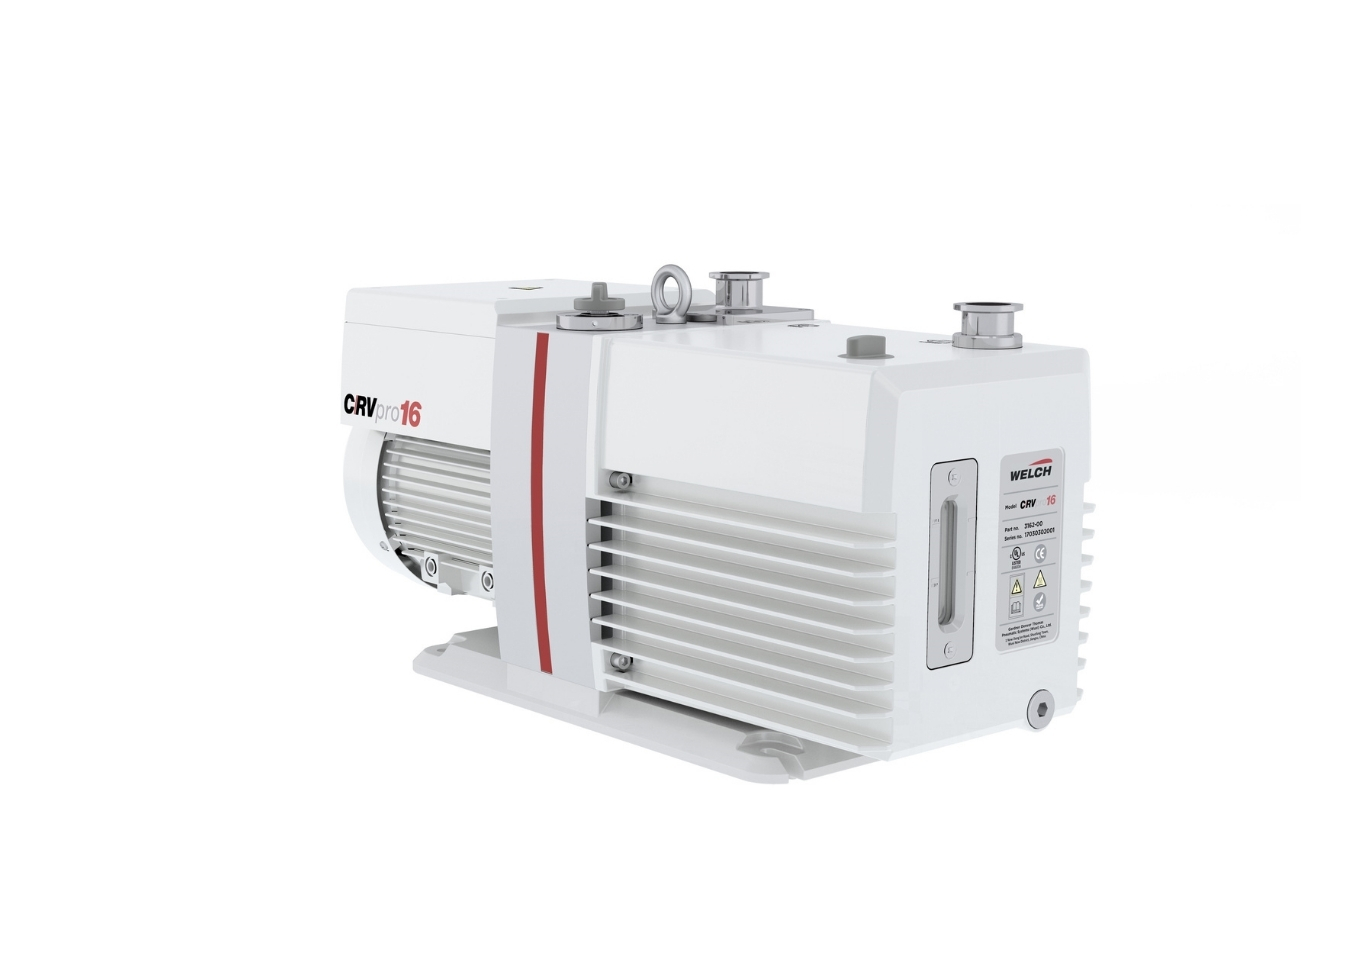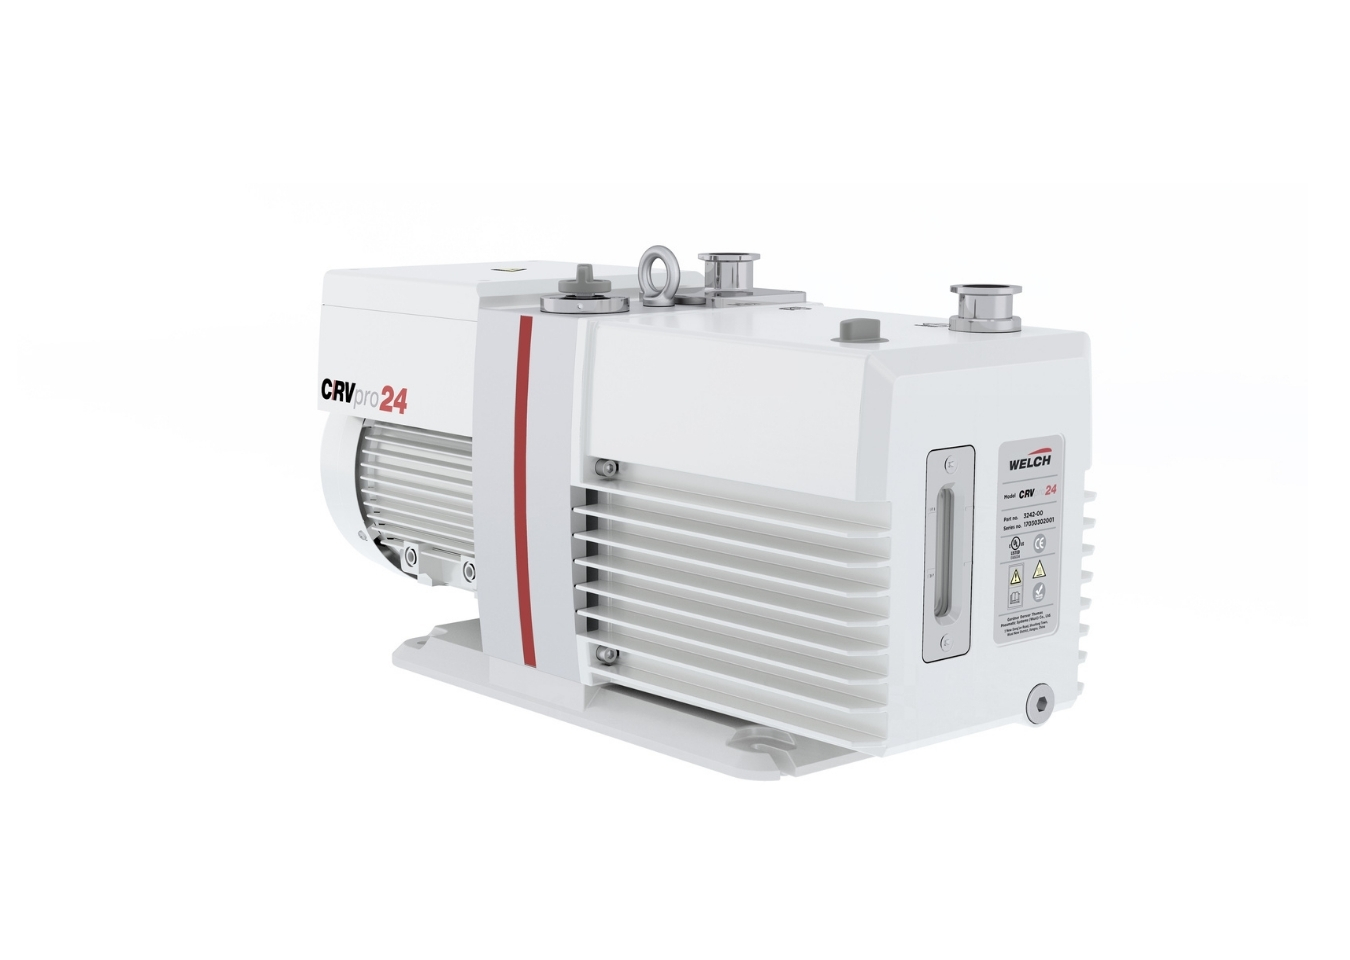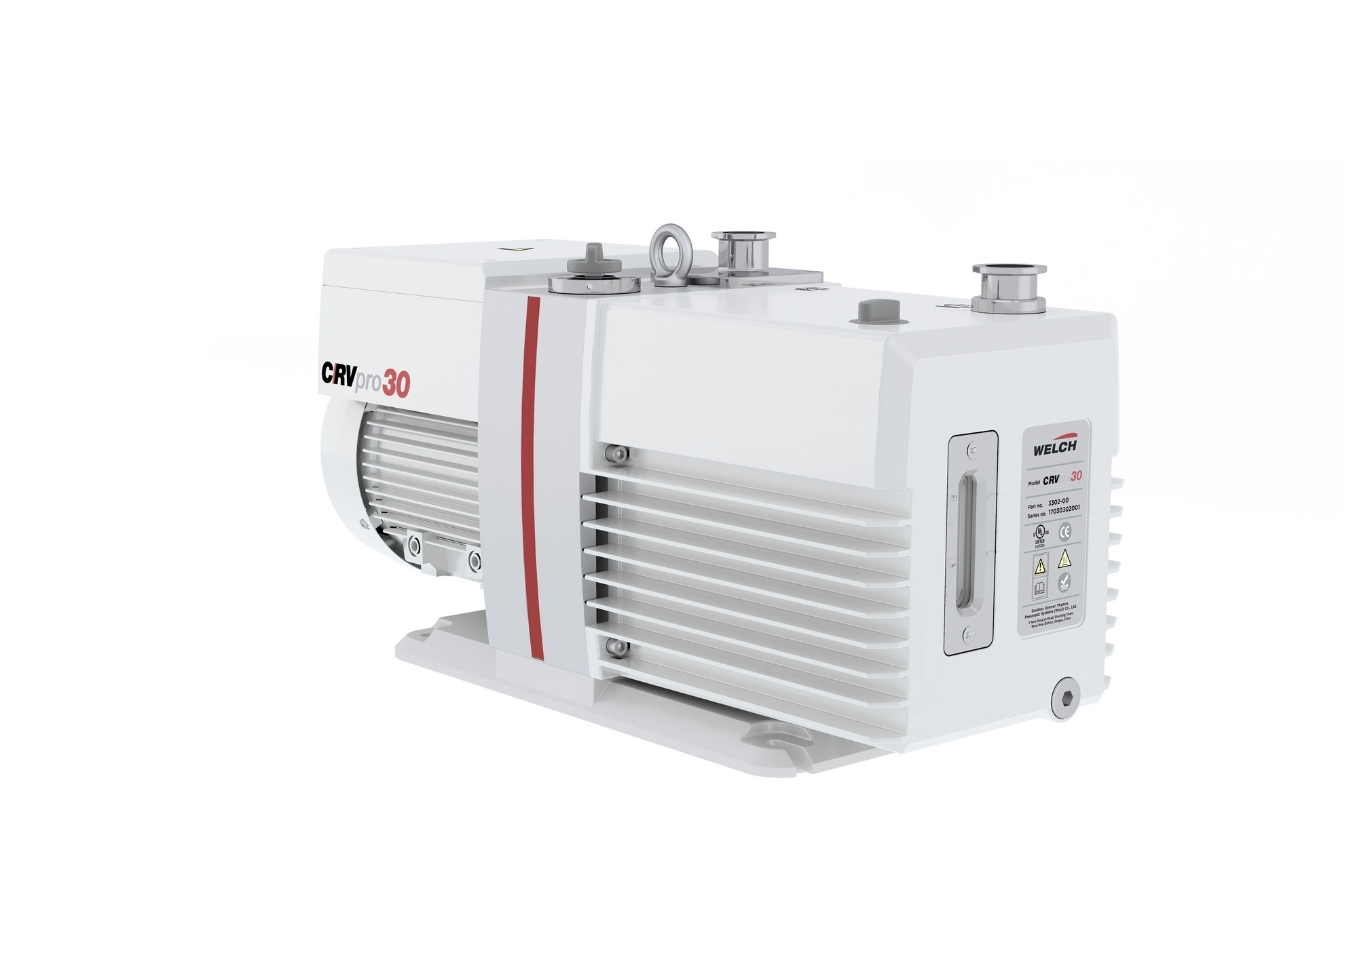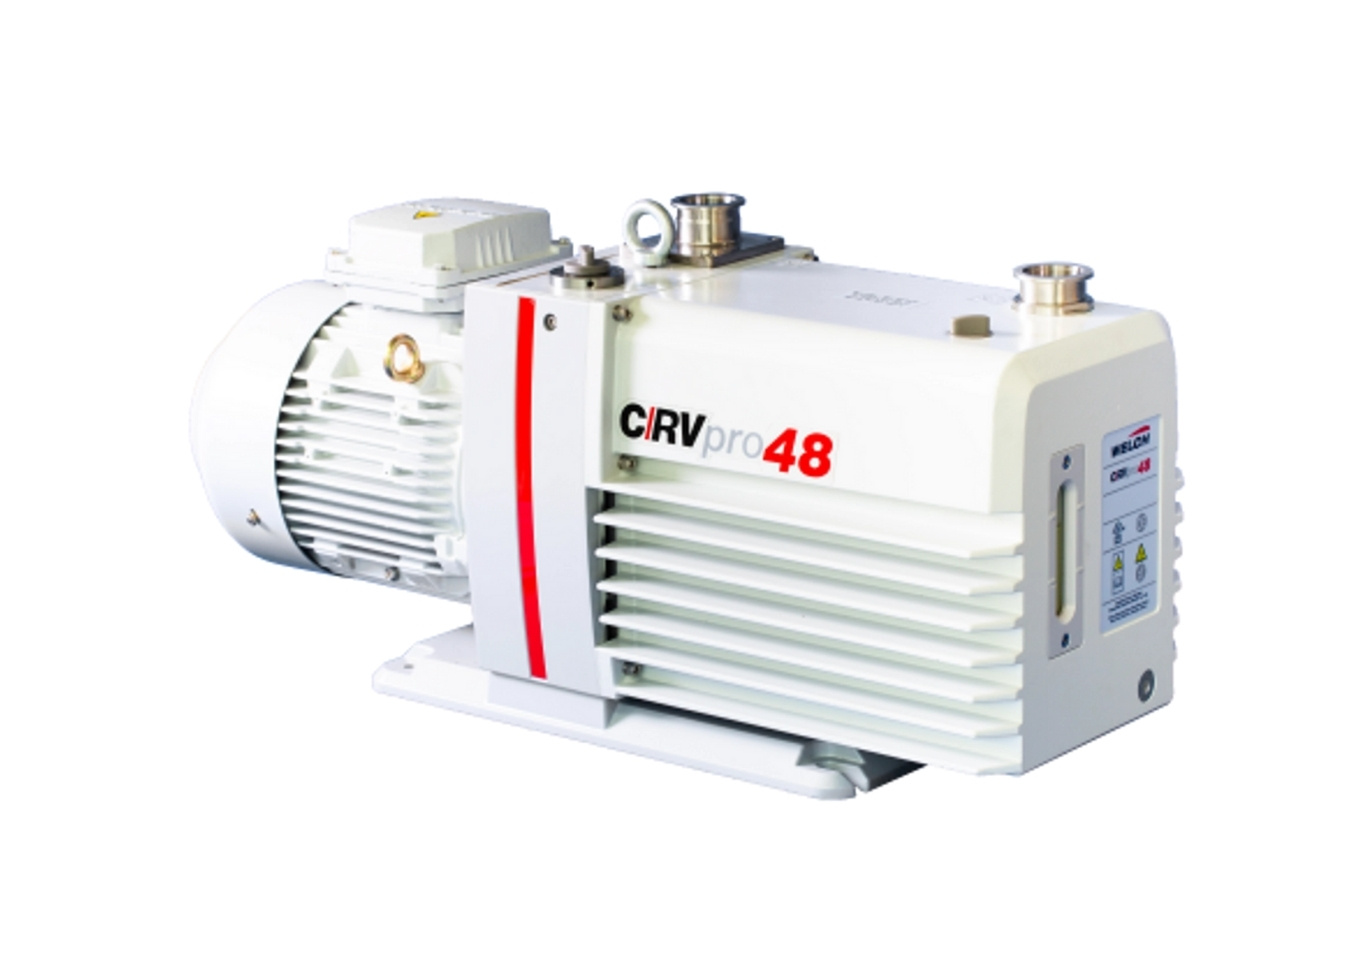
Two-stage rotary vane vacuum pumps
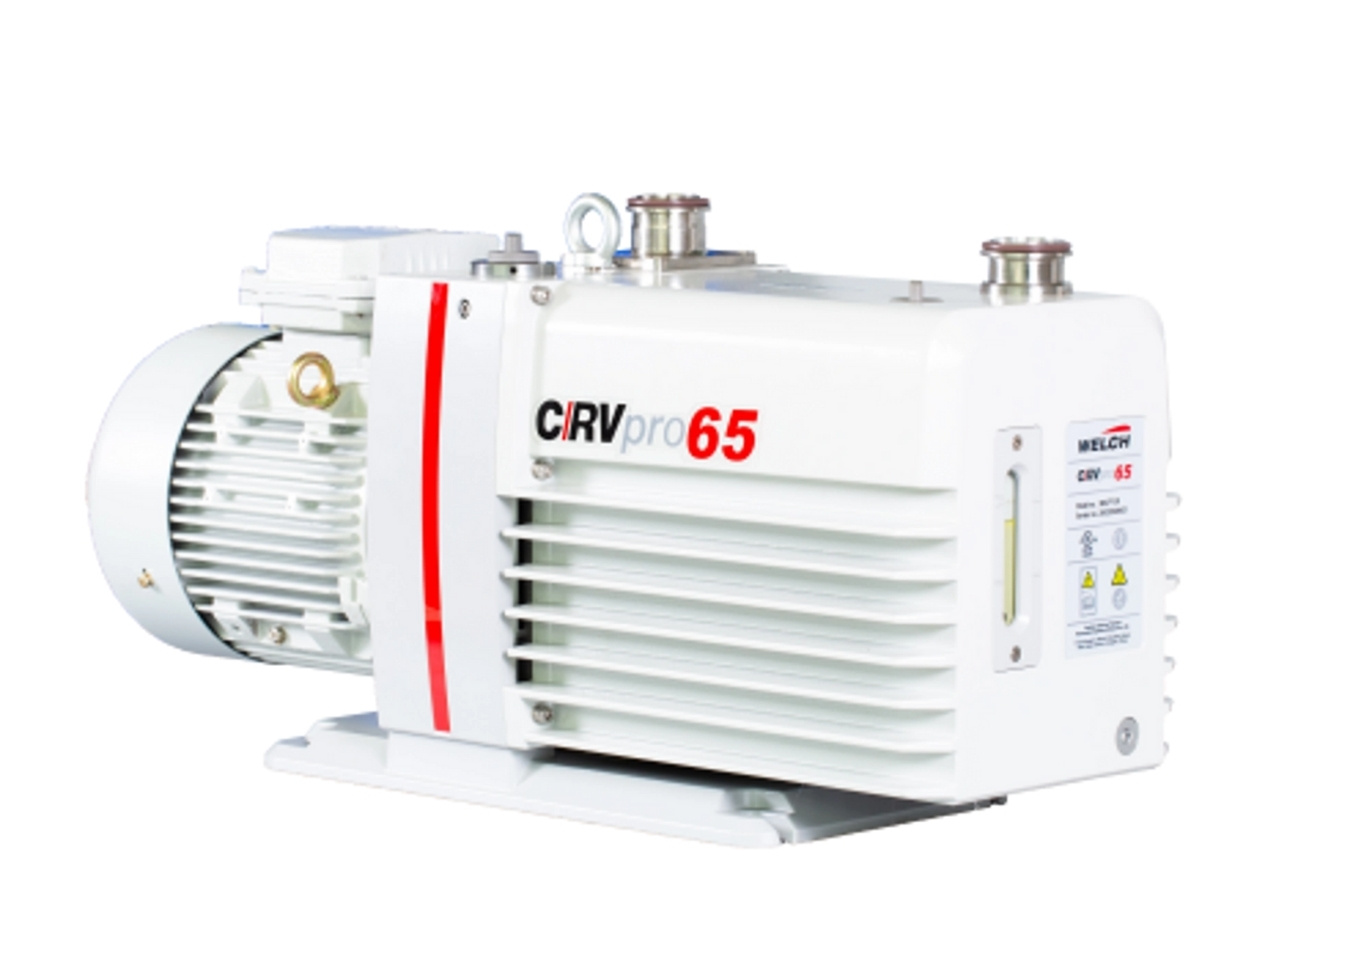
Welch Rotary Vane Vacuum Pumps – precision and performance in perfect balance.
Using rotating vanes, these pumps create and maintain stable vacuum conditions – the very foundation of modern vacuum technology. This enables progress across research, industry, and manufacturing.
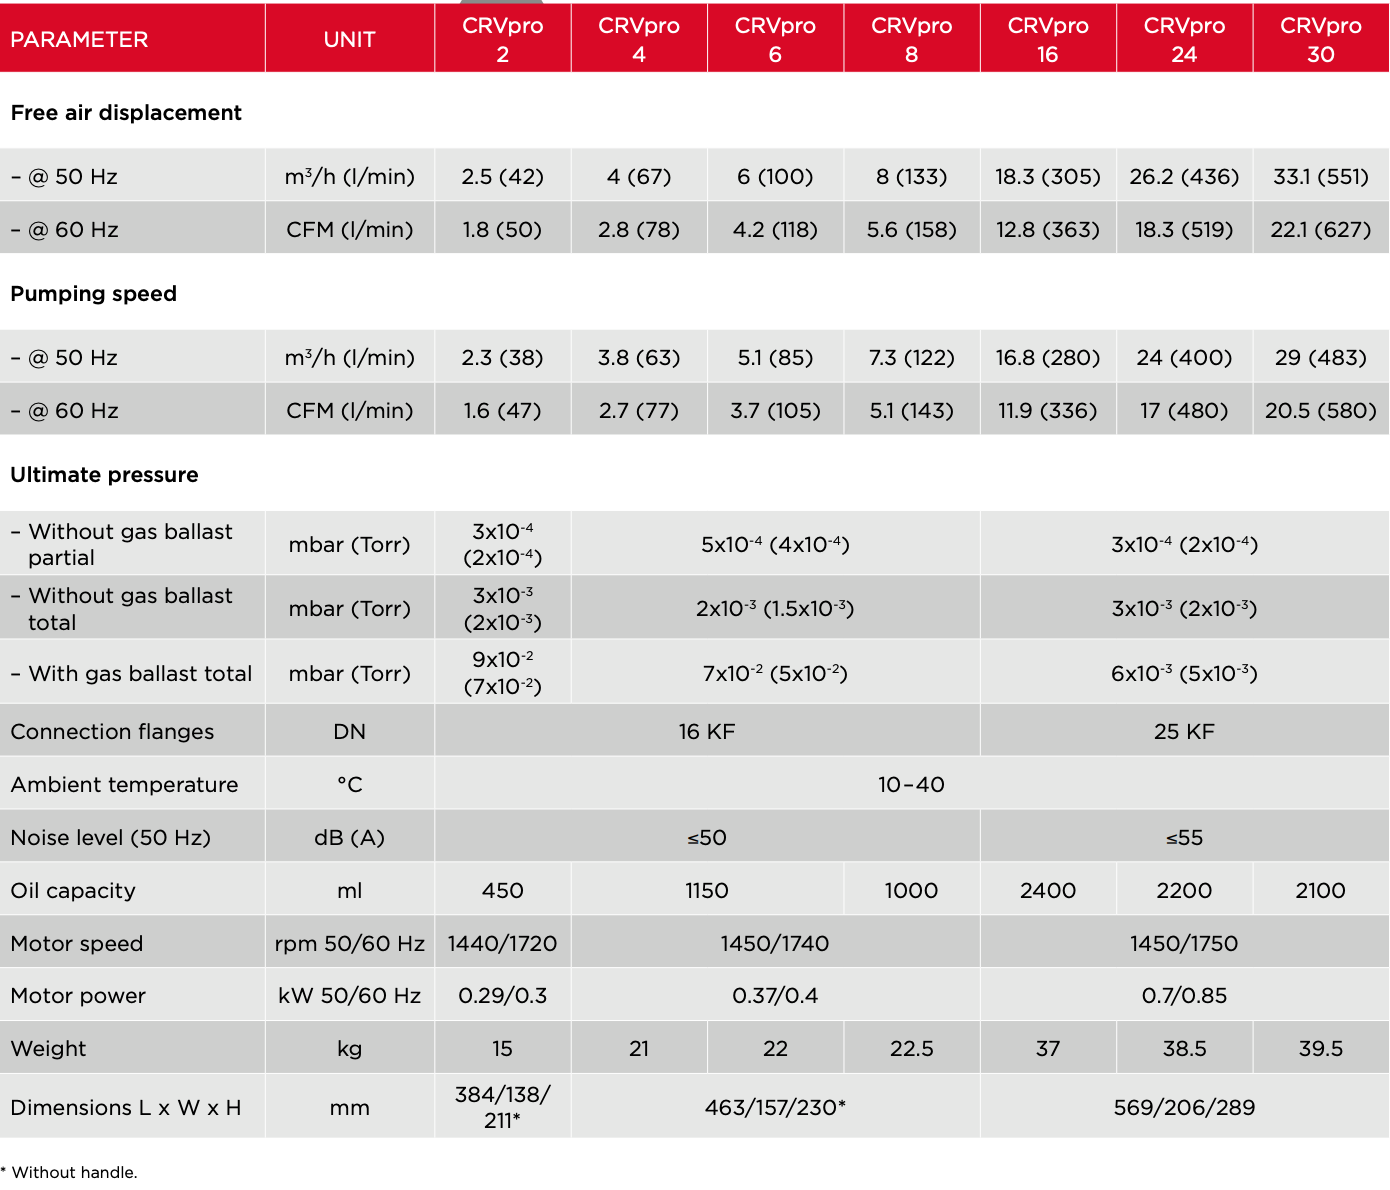
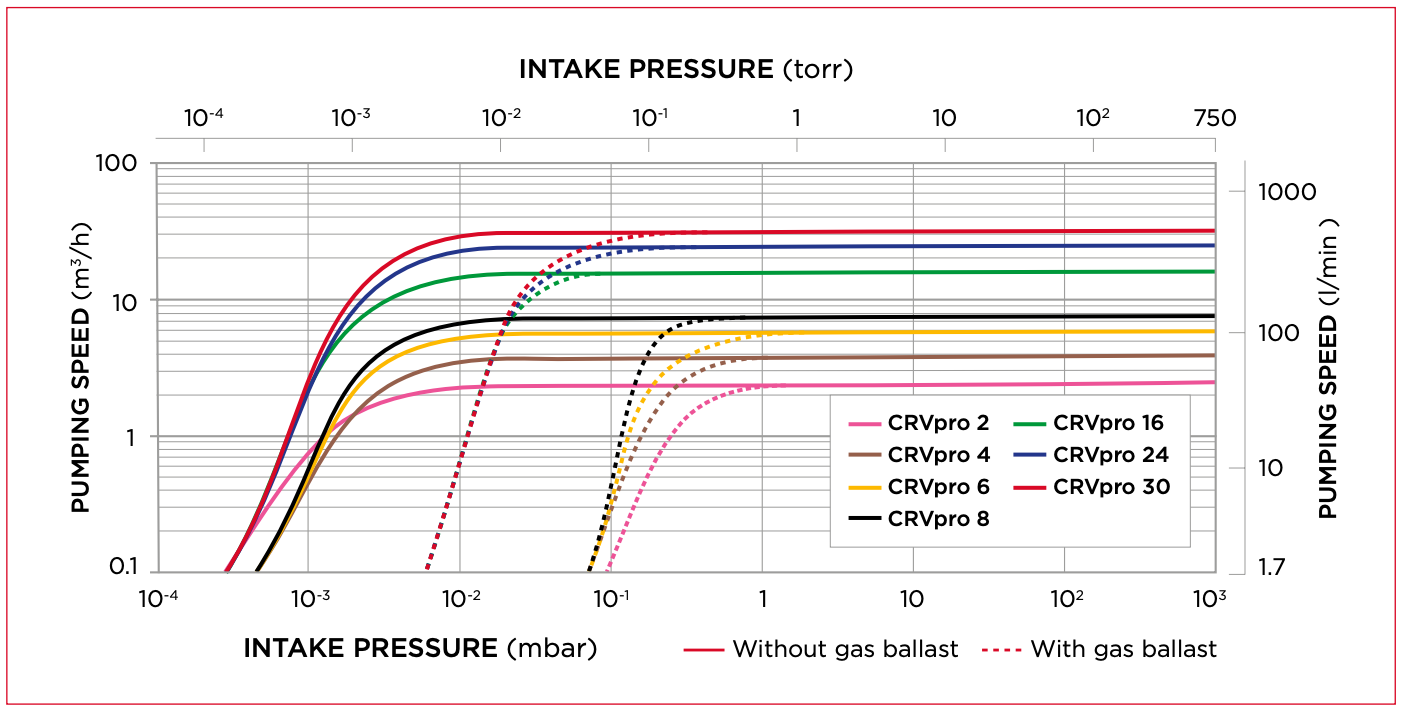
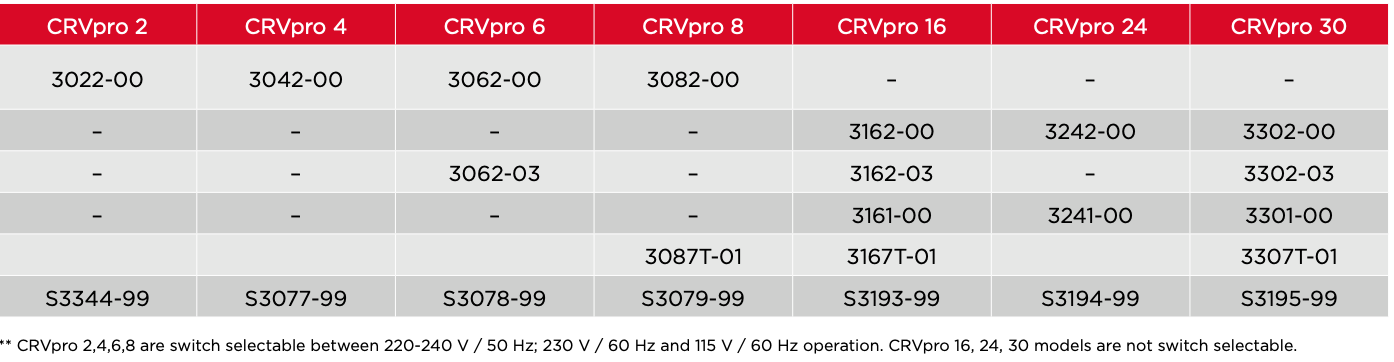
Welch offers a wide selection of models, from low- to high-capacity solutions, each engineered to meet specific vacuum requirements. The pumps deliver speeds from 2 to 64 CFM (3.4–108.7 m³/h) and achieve vacuum levels down to 0.0003 Torr.
The result is a combination of precision, reliability, and innovation that sets the standard for laboratories, production environments – and beyond.
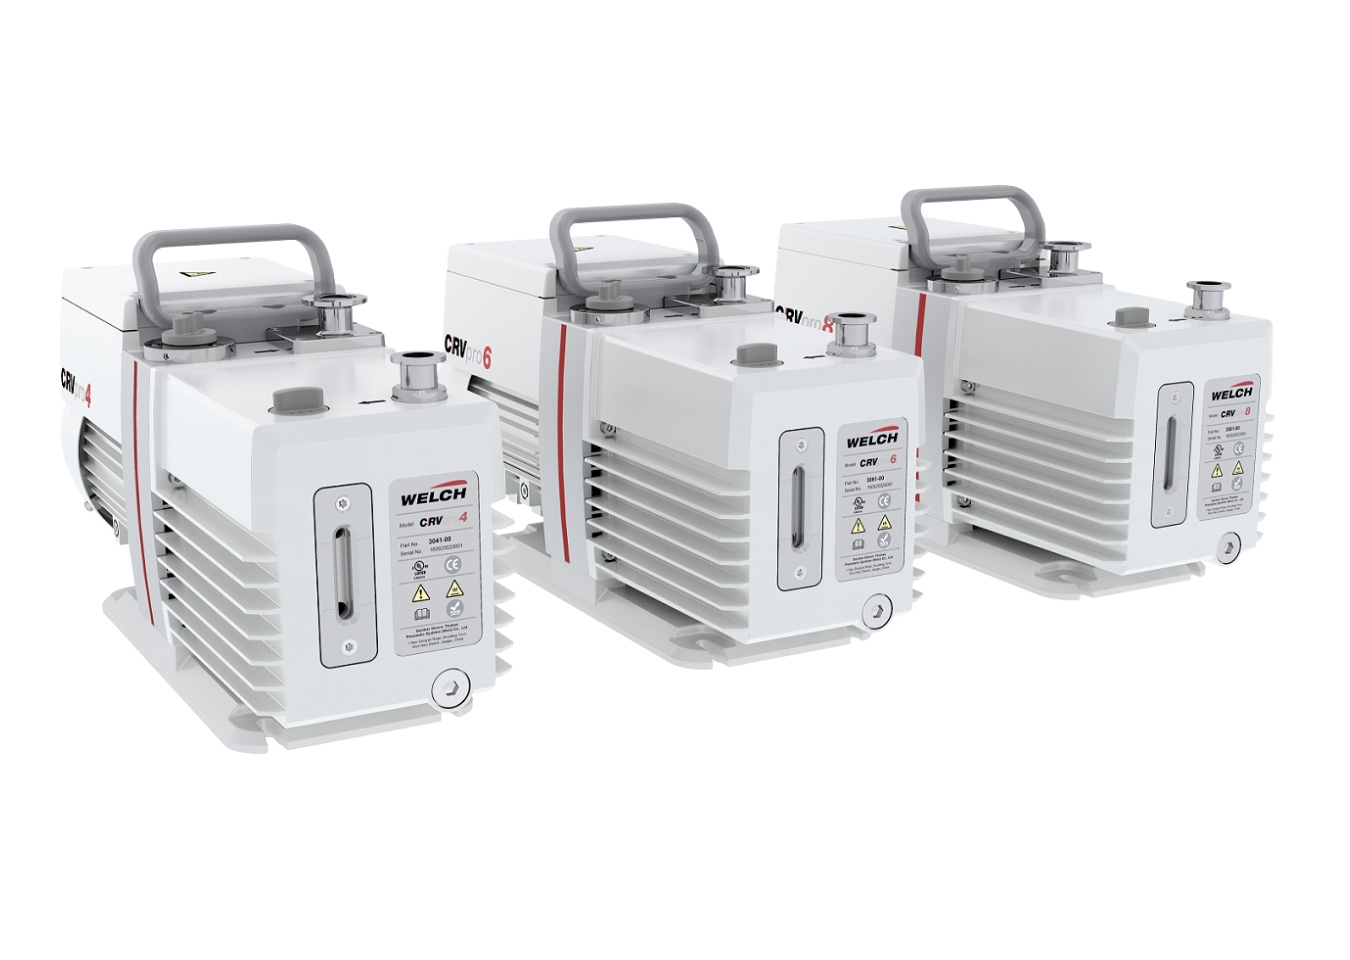
The CRVpro family includes all the features you’d expect in a direct drive rotary vane pump: gas ballast, forced oil lubrication, anti-suckback mechanism and thermal overload protection.
CRVpro vacuum pumps can be used for applications such as:
- freeze drying
- vacuum ovens
- schlenk line
- backing turbo molecular pumps
- degassing
- vessel/chamber evacuation
Direct drive pumps are not recommended for filtration, aspiration, drying electrophoresis gels, or other applications requiring sustained operation above 30 torr.
See all our Welch vacuum pumps.
Download the CRVpro brochure.